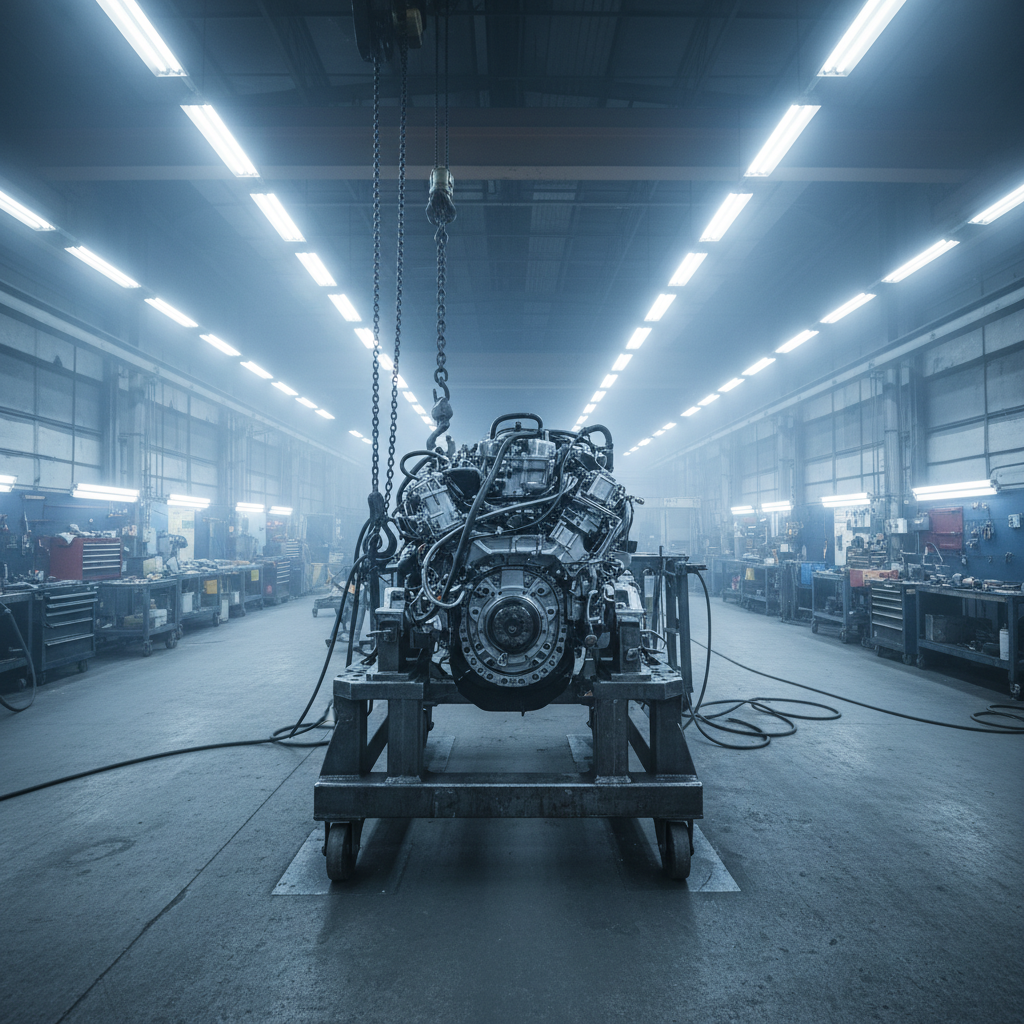
Marine assembly bay interior — partially assembled stern drive on rolling jig, overhead crane chains, fluorescent shop lights cutting through grinding dust haze

Hull to helm, assembled right.

Berth Marine Assembly — Commercial Fabrication & Integration

Receiving InspectionFixture & AlignmentStructural WeldingMechanical IntegrationQuality VerificationSea-Trial SupportAWS D1.1 CertifiedMIL-SPEC TolerancesUSCG-Compliant DocumentationCommercial Fleet RefitNaval Architecture LiaisonISO 9001 Process ControlReceiving InspectionFixture & AlignmentStructural WeldingMechanical IntegrationQuality VerificationSea-Trial SupportAWS D1.1 CertifiedMIL-SPEC TolerancesUSCG-Compliant DocumentationCommercial Fleet RefitNaval Architecture LiaisonISO 9001 Process Control

The Assembly Sequence

Six stages.
Every step documented.

Each card is a stage in the assembly workflow — what happens, what tolerances are held, and what the client receives at the end of it.
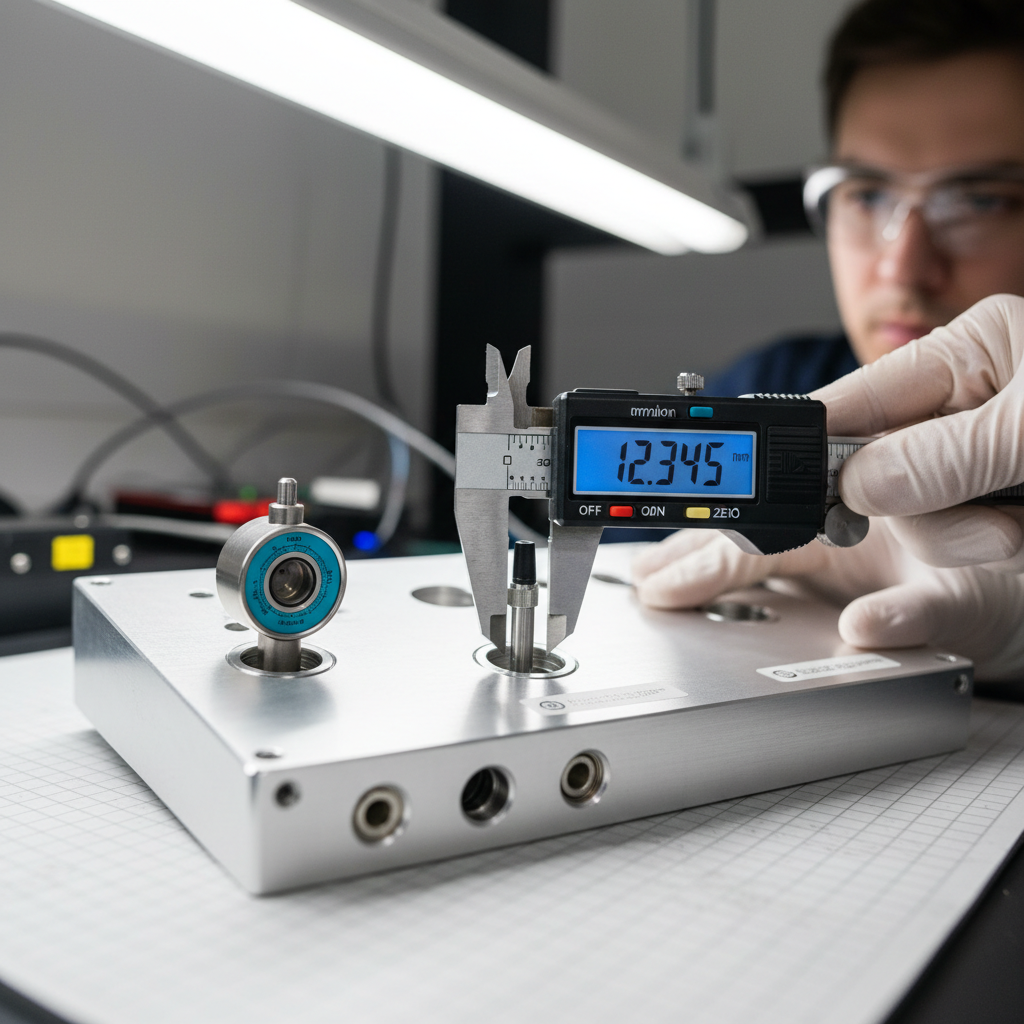
Technician measuring steel component with calipers against engineering drawing on workshop bench
01 — Receiving

Receiving Inspection

Every component entering the shop is logged against the bill of materials, measured against drawing callouts, and photographed before it touches a fixture. Dimensional deviations above 0.005″ are flagged and held pending client authorization — nothing moves forward on assumption.

±0.005″ dimensional hold

Docs:Receiving log, photo record, BOM reconciliation sheet

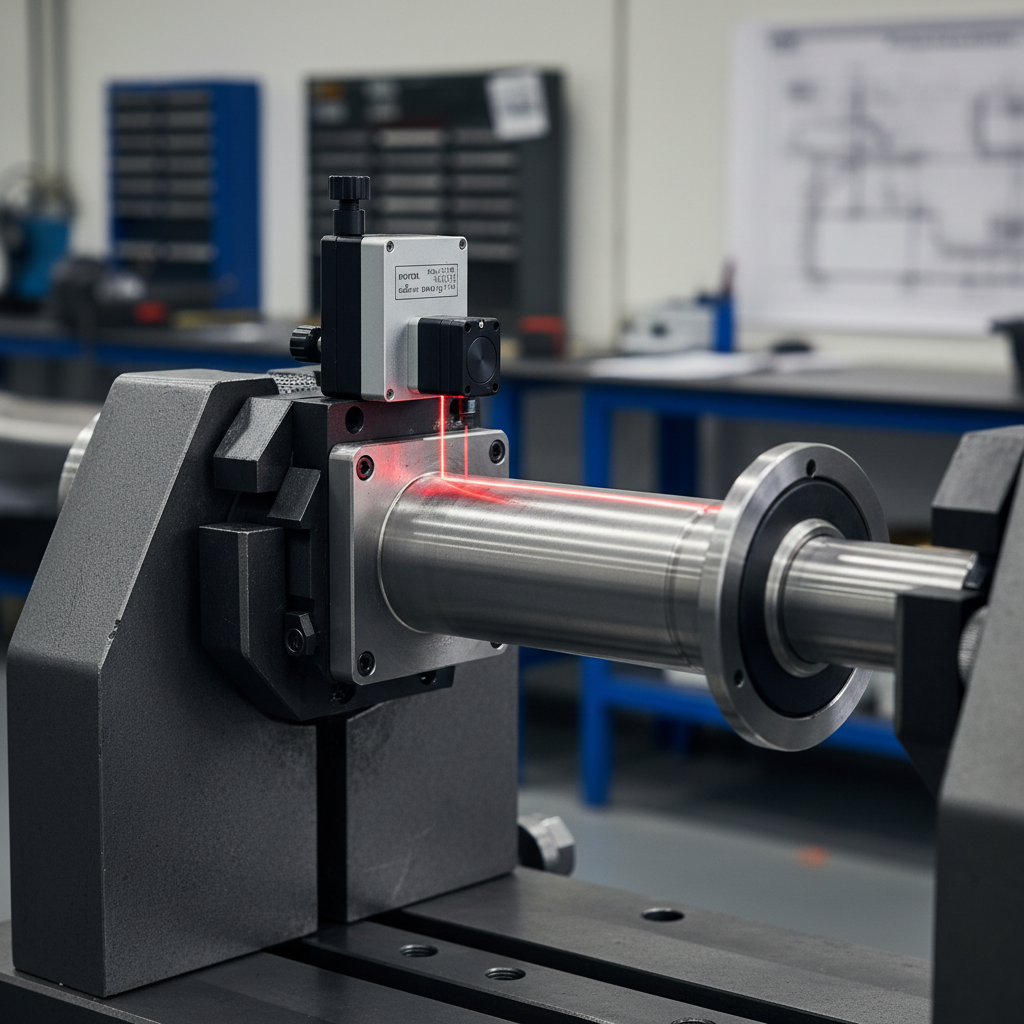
Laser alignment tool mounted on marine drive shaft in industrial workshop fixture
02 — Setup

Fixture & Alignment

Assemblies are set to certified fixtures and dialed in with laser alignment tools. Shaft centerlines, engine mounts, and hull datum points are verified before any fastener is torqued. This is where tolerance stack-up gets caught — not in the water.

Shaft alignment ±0.002″ TIR

Docs:Fixture setup sheet, laser alignment printout, datum verification checklist

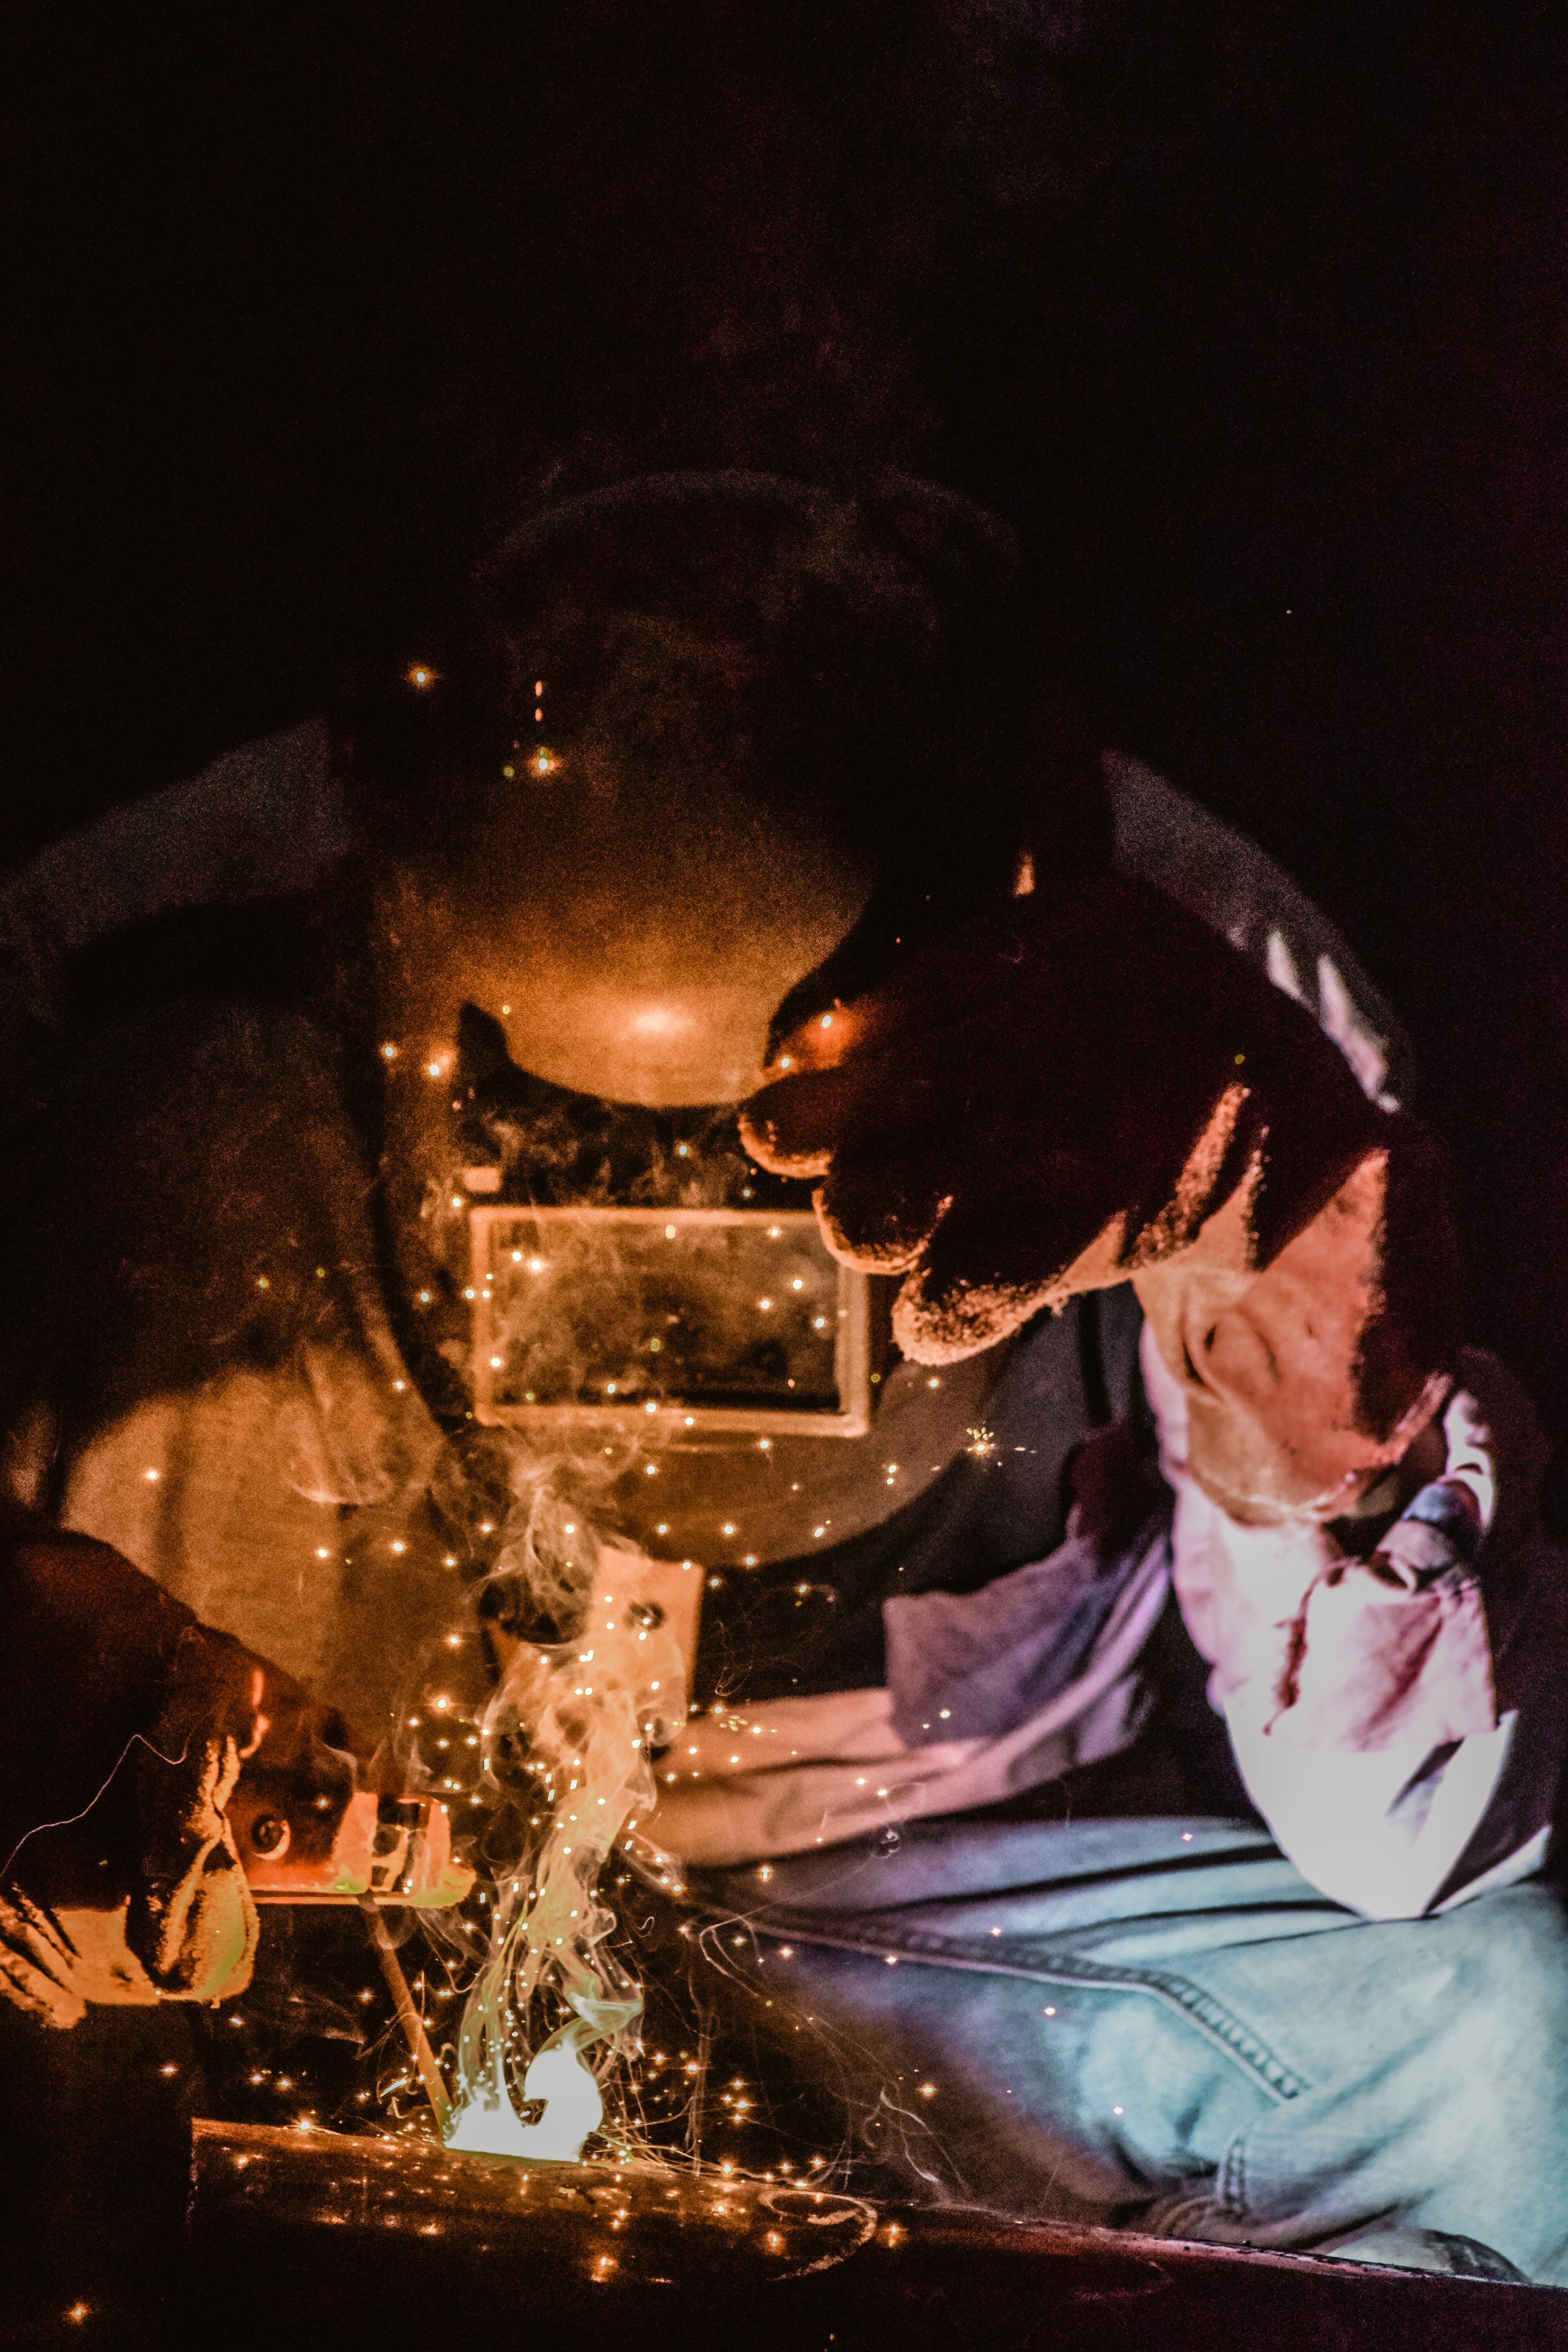
Welder in full protective gear arc welding steel hull section with bright orange weld arc visible
03 — Fabrication

Welding & Fabrication

Structural welds are performed to AWS D1.1 by certified welders. Marine-grade stainless and aluminum work follows D1.2. Every weld is visually inspected; critical joints are UT or dye-penetrant tested per the drawing specification. No contractor shortcuts — the same hands that weld it sign the inspection record.

AWS D1.1 / D1.2 certified; fillet throat ±10%

Docs:Welder certification records, weld map, NDT reports

Technical Resource

Assembly Spec Guide

46 pages covering fixture tolerances, weld procedure specifications, torque tables, NDT acceptance criteria, and documentation requirements for commercial marine assemblies. Written for boatyard managers and naval architects who need the actual numbers, not a sales deck.
Download the GuidePDF · 46 pages · Free
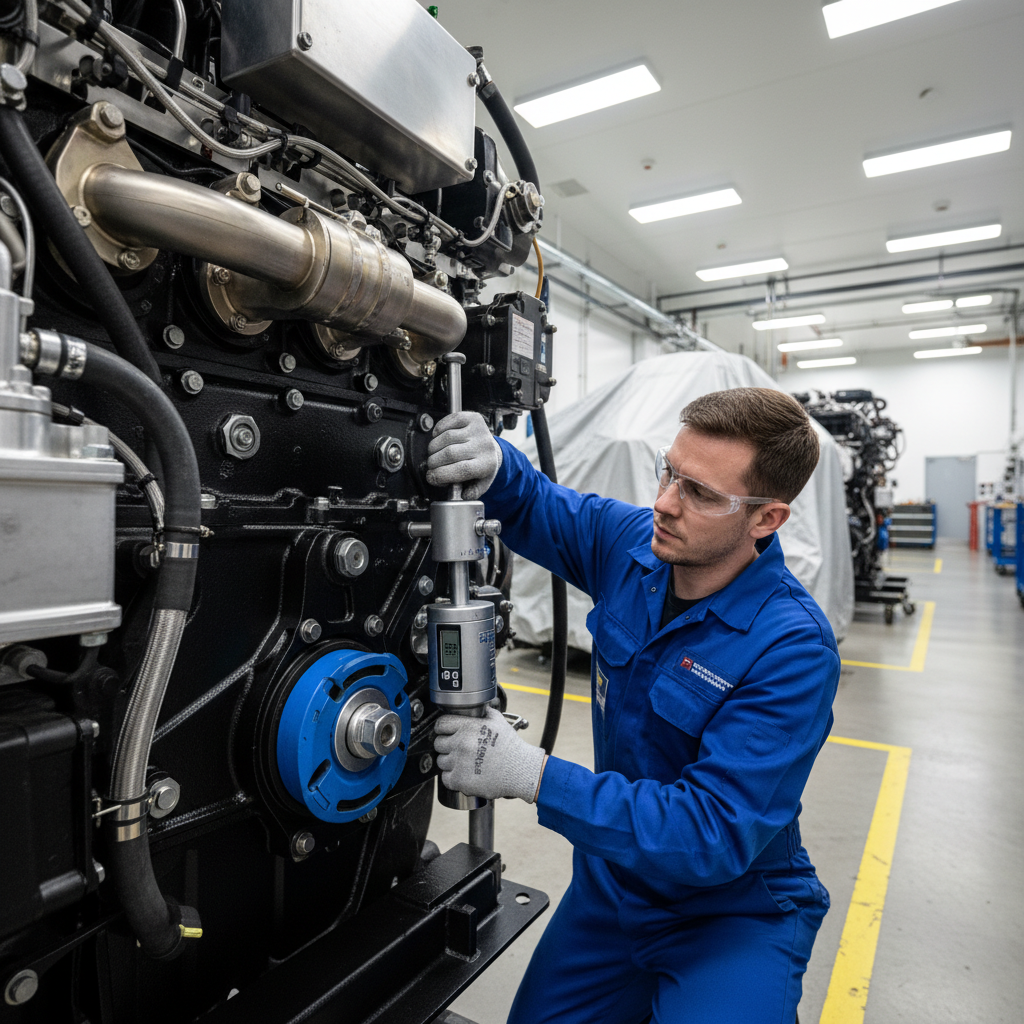
Technician torquing marine engine mount bolts with calibrated torque wrench in assembly bay
04 — Integration

Mechanical Integration

Engine mounts, drive couplings, seacocks, and through-hull fittings are assembled to torque spec with calibrated tooling. Fastener grades are verified against the drawing callout. Hydraulic and fuel lines are pressure-tested before any enclosure is closed. Nothing gets buried without a signed test record.

Torque to drawing spec ±5%; proof pressure per ABYC

Docs:Torque log, pressure test records, assembly sequence photos

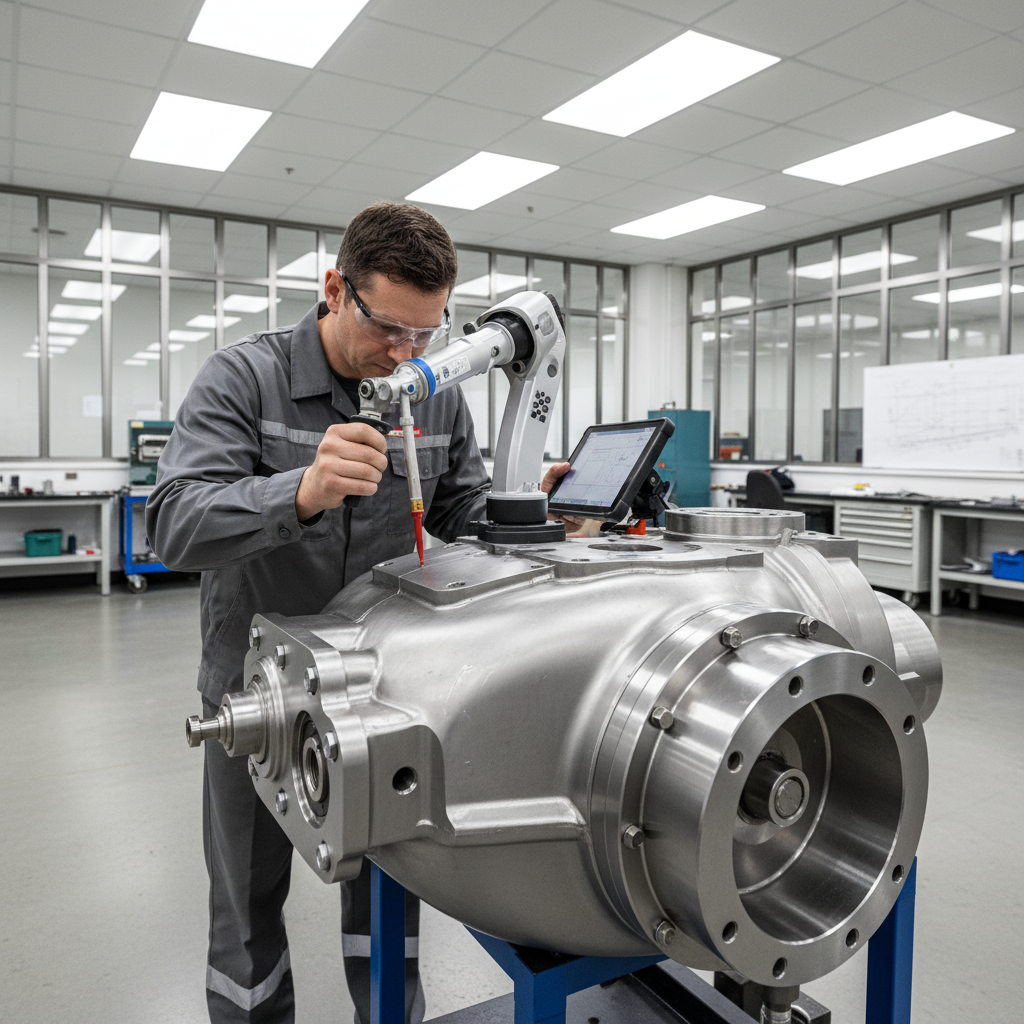
Quality inspector using coordinate measuring arm on finished marine assembly component
05 — Verification

Quality Verification

Final dimensional inspection is run against the drawing package using a coordinate measuring arm. Every critical characteristic gets a pass/fail result logged to the job traveler. First-article reports are generated in FAIR format on request. Nothing ships without a completed traveler signed by the lead technician.

CMM inspection ±0.003″; all drawing CTQs captured

Docs:Completed job traveler, CMM report, first-article inspection report (optional)

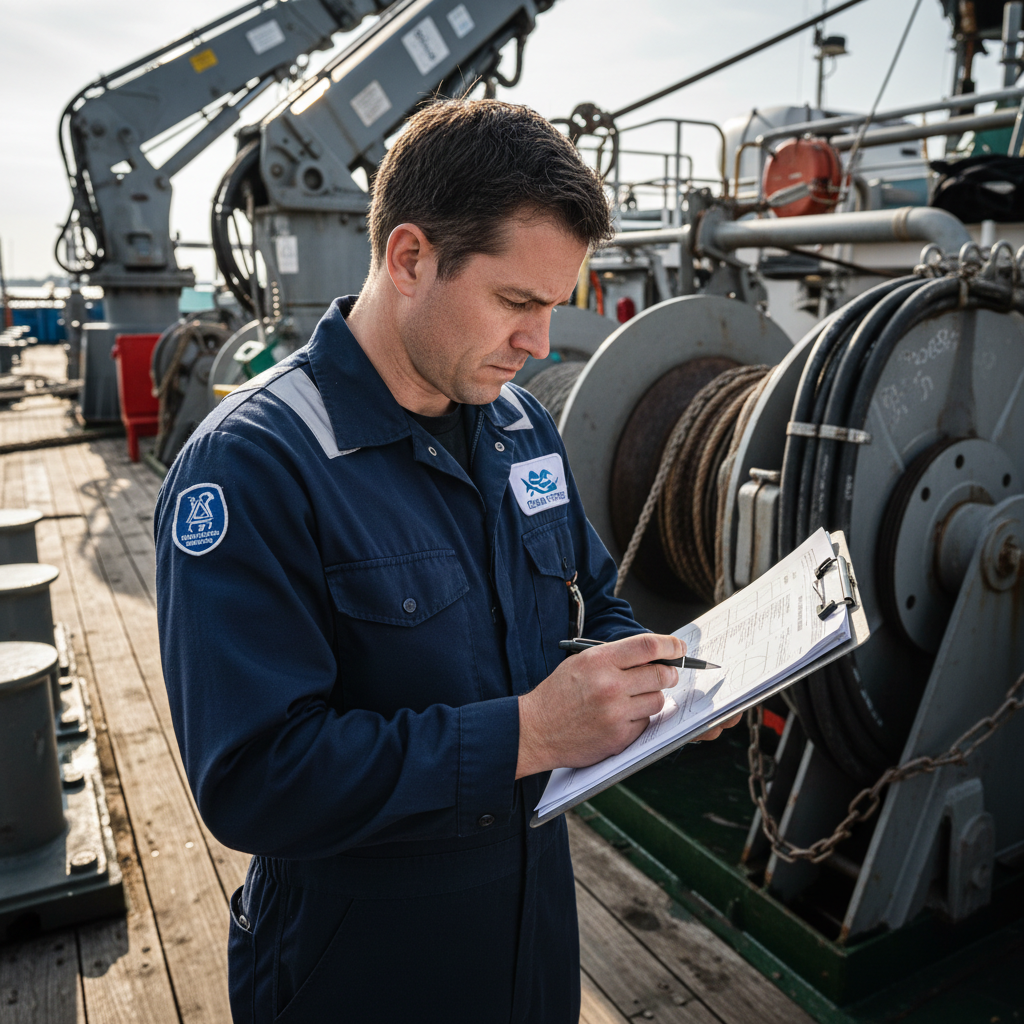
Marine technician on vessel dock reviewing commissioning data on clipboard during sea trial
06 — Delivery

Sea-Trial Support

Berth technicians are available dockside for first commissioning. We carry the job traveler onto the vessel, verify installation interfaces, and observe initial run-up. Vibration and temperature readings are logged at the first sea trial. If something reads outside spec, we are already there to diagnose it.

Vibration analysis per ISO 10816; thermal imaging at first run

Docs:Commissioning report, sea-trial data log, thermal image archive

Spec Guide + Individual Process PDFs

Get the technical
documentation.

Fill out the form to receive the full Assembly Spec Guide by email. If you only need one specific stage, note your vessel type and we will send the relevant process PDF directly — no full guide required.

Individual Process PDFs — Email Only

Receiving & Inspection Protocol
Fixture & Alignment Procedures
Weld Procedure Specifications (WPS)
Torque & Pressure Test Standards
CMM Inspection Criteria
Commissioning & Sea-Trial Checklist
Request Documentation

No sales calls. Just the documentation you asked for.